No products in the cart.
USP 790 Visual Inspection India: Essential Guide for Pharma Excellence
Why visual inspection deserves more attention
A clear injectable product does not automatically mean a defect-free product. A tiny glass fragment, metal particle, fiber, elastomeric fragment or other visible contaminant may be difficult to detect, but its presence can create a serious product-quality and patient-safety concern.
For pharmaceutical manufacturers in India, visual inspection is therefore much more than a final packaging-line activity. It is an important part of the quality control strategy for injectable medicines. It requires suitable inspection conditions, trained personnel, well-defined defect standards, documented procedures and a consistent approach to identifying and rejecting defective units.
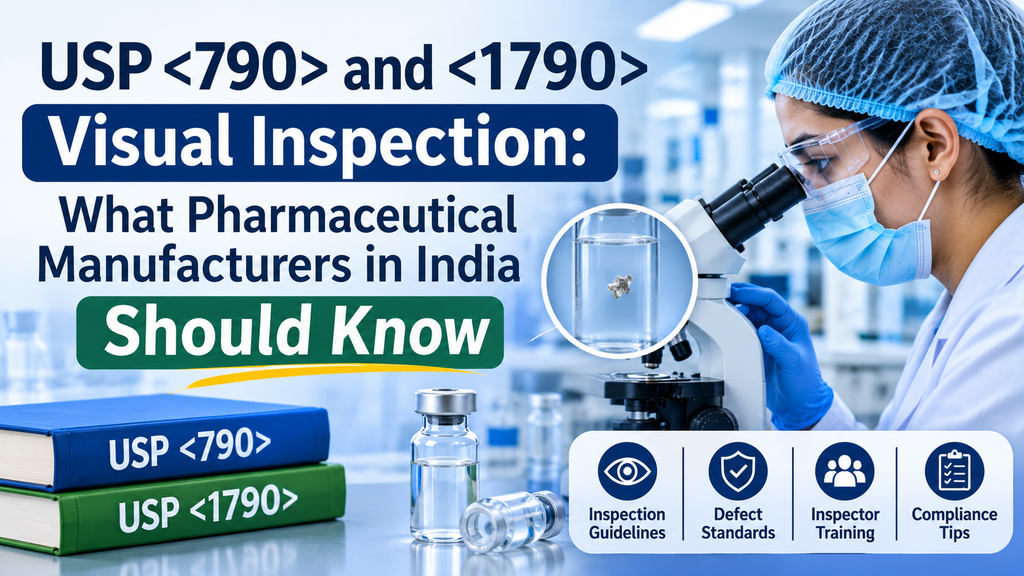
Two important United States Pharmacopeia (USP) chapters help manufacturers understand this subject: USP <790>, Visible Particulates in Injections, and USP <1790>, Visual Inspection of Injections.
Although the chapter numbers look similar, their purposes are different. USP <790> addresses visible particulate inspection and the expectation that injectable products should be essentially free from visible particulates. USP <1790> provides broader guidance on developing, evaluating and maintaining an effective visual inspection programme.
For Indian manufacturers supplying domestic and international markets, understanding these chapters can help strengthen inspection practices, prepare teams for customer and regulatory audits, and improve the consistency of manual and automated inspection systems.
This article explains the key concepts, practical implementation considerations and the role of KNAPP kits in visual inspector training and qualification.
1. Understanding USP <790> and USP <1790>
Before improving a visual inspection programme, manufacturers should understand what each chapter covers and how the two work together.
What is USP <790>?
USP <790> is titled Visible Particulates in Injections. It addresses the visual inspection of products intended for parenteral administration to identify visible particulate matter.
Particulate matter generally refers to extraneous, mobile, undissolved particles, other than gas bubbles, that are unintentionally present in a solution.
Examples include:
- Glass particles
- Metal particles
- Fibres
- Elastomeric fragments
- Precipitates
- Other foreign particles
The chapter uses the concept of a product being “essentially free” from visible particulates. This does not mean that manufacturers can ignore occasional defects or accept contamination without investigation. It means the inspection process must be designed and performed according to the applicable compendial expectations and acceptance criteria.
Manufacturers should consult the current official USP-NF text and applicable product requirements when establishing their procedures.
What is USP <1790>?
USP <1790> is titled Visual Inspection of Injections. It provides broader guidance on the development and implementation of an effective inspection process.
It discusses several important areas, including:
- Manual visual inspection
- Semi-automated and automated inspection
- Inspection process capability
- Defect classification
- Preparation of defect standards
- Probability of Detection (PoD)
- Inspector training and qualification
- Requalification
- Inspection lifecycle management
- Trending and interpretation of inspection results
An important concept in USP <1790> is that visual detection is probabilistic. The ability to detect a particle depends on factors such as its size, shape, colour, density, movement, the formulation and the container design.
For example, a dark particle may be relatively easy to identify in a clear solution, while a transparent glass fragment may be much more difficult to observe under the same conditions.
USP <790> vs USP <1790>: Key differences
| Area | USP <790> | USP <1790> |
|---|---|---|
| Main focus | Visible particulates in injections | Broader visual inspection programme |
| Primary purpose | Addresses visible particulate inspection expectations | Provides guidance for inspection development and qualification |
| Inspection methods | Addresses visual inspection of injectable products | Discusses manual, semi-automated and automated methods |
| Defect standards | Relevant to inspection expectations | Discusses preparation and use of defect standards |
| Inspector qualification | Not its central focus | Discusses training and qualification |
| Inspection performance | Focuses on visible particulate acceptance | Discusses process capability and detection probability |
Practical takeaway: USP <790> and USP <1790> should be understood together. One addresses visible particulate expectations, while the other helps manufacturers build a more comprehensive inspection strategy.
2. Why visual inspection is important for pharmaceutical manufacturers in India
India is a major pharmaceutical manufacturing and export market. Injectable products manufactured in India may be supplied to hospitals, healthcare institutions and regulated markets worldwide.
This makes reliable visual inspection important for manufacturers of:
- Small-volume parenterals (SVPs)
- Large-volume parenterals (LVPs)
- Liquid injectable formulations
- Lyophilized products
- Prefilled syringes (PFS)
- Cartridges
- Other sterile products in appropriate container systems
A weak inspection programme can create several operational and quality challenges.
Patient safety
Visible foreign particles in injectable products can create patient-safety risks. Manufacturers must therefore establish appropriate controls to prevent, detect, investigate and reduce particulate contamination.
Product quality
An effective inspection process helps identify visible particles, container defects, closure problems and other relevant defects before products are released.
Regulatory and customer audit readiness
Auditors may want to understand how manufacturers establish inspection conditions, train inspectors, qualify inspection processes and maintain supporting records.
Simply stating that operators have completed visual inspection training may not demonstrate that the inspection process is capable and consistently performed.
Reduced rejection and reinspection
Inconsistent inspection performance can result in two problems:
- False acceptance: A defective unit is accepted when it should have been rejected.
- False rejection: An acceptable unit is rejected because of inconsistent interpretation or inspection technique.
Both outcomes can affect product quality, manufacturing efficiency and batch disposition.
A structured training and qualification programme helps manufacturers evaluate inspection performance and reduce unnecessary variation.
3. Important elements of an effective visual inspection process
A successful visual inspection programme requires more than a trained operator and a suitable light source. Several factors influence the inspection outcome.
3.1 Suitable lighting and background
Lighting conditions should be established and controlled according to the applicable procedure and product characteristics.
For manual inspection, manufacturers should consider:
- Suitable illumination at the inspection point
- Appropriate black and white backgrounds
- Consistent working conditions
- Controlled inspection distance and positioning
- Equipment maintenance and calibration or verification, as applicable
- Suitable arrangements for different formulations and containers
Black and white backgrounds help inspectors identify particles with different colours and contrast characteristics.
For example:
- A white fibre may be more visible against a dark background.
- A black particle may be easier to identify against a white background.
- A transparent particle may require careful movement and observation to become noticeable.
The inspection setup should be established through a documented, product-appropriate procedure rather than relying on operator preference.
3.2 Correct handling of containers
The way an inspector handles a vial or other container can influence particle movement and visibility.
Training should cover:
- Proper vial holding techniques
- Gentle swirling and inversion, where appropriate
- Avoiding unnecessary bubble formation
- Consistent inspection positioning
- Careful observation against the specified backgrounds
- Appropriate handling of clear and coloured solutions
Different formulations may behave differently during inspection. A clear aqueous solution, an oily formulation and a coloured solution may require different inspection considerations.
3.3 Inspection duration and operator fatigue
Human visual performance can be affected by fatigue, repetitive tasks and poor working conditions.
Manufacturers should establish suitable inspection durations, breaks and eye-rest arrangements through their procedures and risk assessments.
Training should also help operators understand the importance of consistent inspection technique rather than rushing through containers to meet production targets.
3.4 Defect classification
A visual inspection programme should define how defects are classified and how inspection decisions are made.
Common categories include:
- Critical defects: Defects that may create a significant risk to patient safety or product quality.
- Major defects: Defects that significantly affect product quality or acceptability.
- Minor defects: Defects with a comparatively lower impact, as defined by the manufacturer’s approved classification system.
Examples of defects used in training and qualification may include:
| Defect category | Illustrative examples |
|---|---|
| Particulate defects | Glass, metal, black particles, white particles and fibres |
| Container defects | Cracks, broken containers and other damage |
| Closure defects | Open seals, damaged rubber stoppers and closure problems |
| Product defects | Wrong solution filling and crystallisation |
| Cosmetic defects | Appearance-related defects and cap-related issues |
The final classification and acceptance or rejection decision must be based on the manufacturer’s approved defect standards, product risk assessment and applicable requirements.
4. What is a KNAPP kit, and why is it useful?
A KNAPP kit is a specialised visual inspection defect or test kit used to support the training and qualification of visual inspectors and, where applicable, the evaluation of automated inspection systems.
It provides controlled examples of defective and acceptable units so that inspection personnel can practise identifying different defect types.
Instead of relying only on classroom explanations or photographs, inspectors can work with physical samples that represent inspection challenges.
Types of defects included in visual inspection kits
Depending on the intended application and kit configuration, defect libraries may include:
- Clear glass particles
- Amber glass particles
- Metal particles
- Black particles
- White particles
- Black fibres
- White fibres
- Hair fibres
- Other customer-specified particles and fibres
Kits may also include containers representing other defect categories, such as cracks, closure defects, crystallisation and cosmetic defects.
Different KNAPP kit applications
1. Defect library kits
These provide a collection of known defect examples. They help inspection teams become familiar with the appearance and characteristics of different defects.
2. Training kits
Training kits may include both defective and good containers. They help inspectors practise identifying defects and making consistent accept-or-reject decisions.
3. Qualification kits
Qualification kits are used as part of a documented inspector qualification programme. Their purpose is to assess whether an individual can perform visual inspection at the defined performance level.
4. Automated inspection machine KNAPP kits
Specialised kits can be used to challenge or qualify automated visual inspection equipment. Their design and application should be suitable for the machine, container and defect types being evaluated.
Why physical defect samples matter
A photograph of a glass particle may help explain what glass contamination looks like. However, it cannot fully reproduce how that particle moves inside a container or how it appears under different lighting conditions.
Physical defect samples help inspectors experience factors such as:
- Particle movement
- Particle contrast
- Particle size and shape
- Visibility against different backgrounds
- Differences between clear and coloured formulations
- Challenges associated with different container types
This makes physical defect libraries useful for practical training and performance evaluation.
5. How KNAPP kits support inspector training and qualification
A structured qualification programme should assess actual inspection performance rather than simply confirm attendance at a training session.
KNAPP kits can support this process when they are designed, controlled and used according to an approved protocol.
Step 1: Identify the inspection requirements
Start by reviewing the products, formulations, container types and manufacturing processes handled by the inspection team.
Consider:
- Clear or coloured solutions
- Liquid or lyophilized formulations
- Vials, cartridges or prefilled syringes
- Likely intrinsic and extrinsic particle types
- Defects that may originate from primary packaging materials, equipment or the manufacturing environment
This assessment helps determine which defect standards are relevant to the qualification programme.
Step 2: Select suitable defect standards
Select defect samples that represent the actual inspection challenges faced by the manufacturing facility.
A useful kit should have a defined purpose and should not contain arbitrary samples that have little relevance to the products being inspected.
Where appropriate, the kit may include different particle materials, colours, fibres and sizes.
Step 3: Train inspectors using practical demonstrations
Training should include both theoretical and practical elements.
Topics may include:
- Fundamentals of USP <790> and USP <1790>
- Inspection techniques
- Tyndall lighting concepts
- Particle visibility
- Vial inversion and swirling
- Background selection
- Inspection duration
- Operator fatigue and eye rest
- Critical, major and minor defect classification
- Intrinsic and extrinsic particles
- Probability of Detection principles
Inspectors should have opportunities to practise with physical samples under controlled conditions.
Step 4: Conduct documented qualification
The qualification protocol should define the test set, inspection conditions, evaluation method and acceptance criteria.
The KNAPP methodology discussed in USP <1790> is associated with evaluating inspection performance using repeated observations and Probability of Detection concepts.
A qualification programme should establish appropriate performance criteria for the relevant defect classes rather than assuming that every defect has the same detectability.
Step 5: Maintain records and requalify inspectors
Qualification records should be maintained according to the site’s quality system.
Useful records may include:
- Inspector identification
- Training completion
- Defect kit identification
- Test-set configuration
- Qualification date
- Inspection results
- Acceptance criteria
- Qualification decision
- Requalification history
- Relevant deviations and corrective actions
Requalification should be performed according to the approved programme, considering factors such as inspection performance, changes in products or processes, and the site’s quality risk assessment.
6. Understanding Probability of Detection (PoD)
One of the important concepts in USP <1790> is Probability of Detection.
Visual inspection is not a perfectly deterministic process. The same particle may be detected during one inspection and missed during another.
PoD is used to describe the frequency with which a particular defect is detected under defined inspection conditions.
A simplified expression is:
PoD = Number of times the defect is detected ÷ Total number of inspection opportunities
For example, suppose a defect sample is presented for 10 inspection opportunities and the inspector identifies it on 8 occasions.
The observed detection frequency is:
8 ÷ 10 = 0.80, or 80%.
This is an illustrative calculation, not a universal qualification acceptance limit.
A meaningful PoD assessment requires a suitable test design, controlled inspection conditions, appropriate sample selection and justified acceptance criteria. A small number of observations may provide limited confidence in the estimated detection probability.
Why PoD is useful
PoD-based assessment can help manufacturers:
- Evaluate inspector performance
- Compare detection capability across defect categories
- Identify difficult-to-detect defects
- Improve training programmes
- Establish more consistent qualification criteria
- Understand inspection process capability
It is important to avoid treating PoD as a single fixed number that applies to every product and defect. Particle characteristics, container design and formulation can all influence detection.
7. Manual vs automated visual inspection
Pharmaceutical manufacturers increasingly use automated visual inspection systems to improve inspection consistency and production efficiency. However, manual inspection continues to play an important role in many manufacturing environments.
| Parameter | Manual visual inspection | Automated visual inspection |
|---|---|---|
| Inspection method | Human observation | Camera and machine-based detection |
| Flexibility | Human judgement can adapt to different visual characteristics | Depends on system configuration and validated algorithms |
| Qualification | Inspector training and qualification | Machine qualification and performance evaluation |
| Main challenge | Human variability and fatigue | System capability and defect recognition limitations |
| Monitoring | Operator records and qualification results | Machine performance and inspection records |
| KNAPP kit application | Training and inspector qualification | Suitable challenge kits for machine evaluation |
Why automated systems still need appropriate test samples
Automated systems must be challenged with representative defects to assess their ability to detect the defects they are intended to identify.
A kit intended for manual inspector qualification may not automatically be suitable for automated machine qualification. Particle movement, container positioning, machine speed, image acquisition and defect characteristics must be considered.
Manufacturers should select test samples and protocols that reflect the intended application of the inspection equipment.
8. How to select the right KNAPP kit supplier in India
Selecting a KNAPP kit supplier is an important decision because the quality and suitability of the defect standards can influence the effectiveness of training and qualification.
Before selecting a supplier, pharmaceutical manufacturers should evaluate the following factors.
1. Defect variety
Check whether the supplier can provide the particle and defect types relevant to your products.
For example:
- Glass particles
- Metal particles
- Black and white particles
- Fibres
- Customer-specific defects
- Good and defective containers
2. Particle sizing and documentation
Ask whether particle and fibre sizes are measured and supported by suitable documentation.
Where particle sizing is provided, understand the measurement method, measurement records and certificate details.
3. Sample preparation and packaging
Defect samples should be prepared and packed appropriately to help preserve their intended condition during storage and handling.
For example, particle and fibre samples may require suitable cleaning, drying, measurement and protective packaging.
4. Formulation and container compatibility
The kit should reflect the intended application.
Consider whether the samples are suitable for:
- Liquid formulations
- Lyophilized products
- Clear glass vials
- Amber glass vials
- Cartridges
- Prefilled syringes
5. Training and technical support
A supplier offering technical guidance and practical training can help manufacturers understand how to use defect standards effectively.
Ask whether support is available for kit handling, inspector training, qualification protocols and technical queries.
6. Kit lifecycle and replacement support
Review the supplier’s recommendations for storage, handling, expiry or reassessment, and replacement of damaged or non-viable samples.
The site’s quality system should also define how kits are inspected, controlled and periodically reviewed.
9. Common mistakes pharmaceutical manufacturers should avoid
Even when a facility has a visual inspection procedure, gaps can develop in day-to-day implementation.
Some common mistakes include:
- Using uncharacterised defect samples: Training with samples that have no suitable identification or supporting information can weaken qualification evidence.
- Treating training attendance as qualification: Completing a training session does not automatically demonstrate inspection capability.
- Ignoring different formulations: A clear solution and a coloured solution may present different inspection challenges.
- Using the same test set indefinitely: Test sets should be reviewed for condition, suitability and continued relevance.
- Ignoring operator fatigue: Poorly managed inspection schedules can affect human performance.
- Failing to investigate inspection trends: Repeated rejection patterns or missed defects may indicate a need for further investigation.
- Using manual kits for automated qualification without assessment: The test samples must be suitable for the intended inspection system.
- Maintaining incomplete documentation: Missing qualification, training or kit-control records can make it difficult to demonstrate programme effectiveness.
A periodic review of these areas can help manufacturers identify improvement opportunities before they become recurring quality issues.
10. A practical checklist for Indian pharmaceutical manufacturers
Use this checklist when reviewing your visual inspection programme:
- Current USP <790> and <1790> requirements and guidance have been reviewed.
- Product-specific inspection procedures are approved.
- Inspection conditions are defined and controlled.
- Black and white backgrounds are available where required.
- Inspectors receive theoretical and practical training.
- Defect categories are clearly defined.
- Suitable physical defect standards are available.
- KNAPP kits are controlled and periodically reviewed.
- Inspector qualification criteria are documented.
- PoD or other appropriate performance evaluation methods are justified.
- Requalification requirements are defined.
- Automated inspection systems are challenged using suitable test samples.
- Inspection results and defect trends are reviewed.
- Deviations and recurring inspection failures are investigated.
This checklist is a practical review aid, not a replacement for the current official pharmacopoeial text or applicable regulatory requirements.
11. How Confianca Pharmazon supports visual inspection programmes
Confianca Pharmazon supports pharmaceutical manufacturers with visual inspection defect kits, training and qualification-related solutions.
Its visual inspection KNAPP kit offerings include manual visual inspection kits for liquid and lyophilized formulations in vial, cartridge and prefilled syringe formats, as well as KNAPP kits for manual and automated inspection applications.
Depending on the kit configuration, available defect examples include:
- Clear and amber glass particles
- Metal particles
- Black and white particles
- Black and white fibres
- Other customer-specified particles and fibres
The company’s documented kit preparation approach includes particle and fibre preparation, cleaning and drying, three-dimensional measurement using high-resolution digital microscopy, and suitable packaging.
Supporting deliverables described for its kits include master certificates, Probability of Detection evaluation sheets and technical support. The supplier also offers training and guidance on manual visual inspector qualification, automated inspection machine qualification and topics associated with USP <790> and USP <1790>.
These services can help manufacturers build a more structured approach to visual inspection training and qualification.
Explore the KNAPP Kit – Visual Inspection Kits for Particles and Particulate Matter to learn more about the available solutions.
Manufacturers should evaluate the kit configuration, documentation and suitability against their own approved procedures and qualification requirements.
Frequently Asked Questions (FAQs)
1. What is the main difference between USP <790> and USP <1790>?
USP <790> addresses visible particulates in injections and the expectation for injectable products to be essentially free from visible particulates. USP <1790> provides broader guidance on visual inspection processes, including defect standards, inspector training, qualification and process capability.
2. Is USP <1790> mandatory for pharmaceutical manufacturers in India?
USP <1790> is a general information chapter that provides guidance on visual inspection of injections. Its applicability should be assessed alongside current Indian Pharmacopoeia requirements, applicable Indian GMP requirements, product-specific approvals, customer commitments and the regulatory expectations of destination markets. Manufacturers should not assume that every recommendation in an informational chapter is automatically a separate statutory requirement in India.
3. What is a KNAPP kit in pharmaceutical manufacturing?
A KNAPP kit is a specialised set of physical defect standards used to support visual inspector training and qualification and, in suitable configurations, automated inspection machine evaluation.
4. Which defects should be included in a visual inspection kit?
Depending on the product and qualification objective, kits may include glass, metal, black and white particles, fibres, container defects and other relevant defect examples. The selection should be based on the manufacturing process and intended application.
5. What is Probability of Detection in visual inspection?
Probability of Detection (PoD) describes how frequently a defect is detected during defined inspection opportunities. It helps manufacturers evaluate detection performance and develop justified qualification criteria.
6. Can KNAPP kits be used for automated visual inspection machine qualification?
Yes, suitable KNAPP kits can be developed for automated visual inspection machine evaluation. However, the kit must be appropriate for the machine, container format, defect characteristics and qualification protocol.
7. How often should visual inspectors be requalified?
There is no single requalification frequency that should be assumed for every facility and product. Manufacturers should establish a documented, risk-based requalification programme consistent with current guidance, their quality system and applicable requirements.
8. Why are certified particle sizes useful in KNAPP kits?
Documented particle sizing helps provide information about the physical characteristics of defect samples. It can support defect identification, training and qualification records. Particle size alone, however, does not determine visibility because colour, shape, density, movement and container characteristics also matter.
9. Are KNAPP kits a replacement for routine 100% visual inspection?
No. KNAPP kits support training, qualification and suitable inspection-system evaluation. They do not replace the manufacturer’s routine inspection process, product-specific controls or required batch inspection activities.
Build a stronger visual inspection programme
USP <790> and USP <1790> provide valuable foundations for understanding visible particulate inspection and developing an effective inspection programme for injectable products.
For pharmaceutical manufacturers in India, the focus should go beyond simply completing visual inspection. A reliable programme should include controlled inspection conditions, appropriate defect standards, practical inspector training, documented qualification, performance evaluation and continuous improvement.
KNAPP kits can play an important role by providing physical defect samples that help inspectors understand real inspection challenges and practise consistent defect identification.
Choosing suitable defect kits, maintaining supporting documentation and establishing a structured qualification programme can help manufacturers strengthen inspection performance and improve confidence in product quality.
If your organisation is planning to improve manual visual inspection, qualify inspectors or evaluate automated inspection systems, explore Confianca Pharmazon’s visual inspection KNAPP kits and training support.
Your trusted partner for pharma skills, systems, and solutions.