No products in the cart.
Knapp Kit Qualification for Automated Visual Inspection: Building Reliable Defect Detection Performance
Introduction
Automated visual inspection has become an important part of pharmaceutical manufacturing, particularly for injectable products packaged in vials, ampoules, cartridges and prefilled syringes.
Modern inspection machines use cameras, sensors, image-processing algorithms and mechanical handling systems to identify visible particles and container defects.
However, installing an automated inspection machine does not automatically guarantee reliable inspection performance.
Manufacturers must demonstrate that the inspection system can consistently identify relevant defects under defined operating conditions.
This is where Knapp Kit Qualification and representative inspection challenge materials become valuable components of a pharmaceutical visual inspection strategy.
A properly designed qualification approach helps manufacturers evaluate defect recognition, detection capability, equipment settings and inspection consistency.
This article explores the role of Knapp kits in automated visual inspection qualification and explains how pharmaceutical manufacturers can establish a structured inspection performance evaluation process.
1. Understanding Automated Visual Inspection in Pharmaceutical Manufacturing
Automated visual inspection systems are designed to examine pharmaceutical containers and identify predefined defects.
Depending on the machine configuration, inspection parameters may include:
- Visible particulate matter.
- Glass fragments.
- Fibres.
- Metallic particles.
- Container cracks.
- Cosmetic defects.
- Stopper and closure-related defects.
- Fill-level irregularities.
The inspection system may use rotating containers, controlled illumination, multiple camera positions and image-processing software.
Each inspection system has its own technical capabilities and limitations.
For this reason, qualification should be based on the actual product, container, machine configuration and intended inspection conditions.
2. Why Knapp Kit Qualification Is Important
A Knapp kit or visual inspection challenge kit provides controlled defect samples for evaluating inspection performance.
These challenge materials can support systematic testing of inspection personnel and automated inspection systems, depending on their design and intended application.
For automated systems, representative challenges help answer important questions:
- Can the machine detect the intended defect?
- Does detection change with particle size?
- Are certain particle types more difficult to identify?
- Does container movement influence detection?
- Are machine settings suitable for the intended product?
- Can inspection results be reproduced?
- Is the qualification supported by appropriate documentation?
A qualification exercise should demonstrate performance against predefined acceptance criteria rather than relying on an informal demonstration.
3. Selecting Representative Defects for Machine Qualification
Challenge samples should reflect the types of defects relevant to the manufacturing process.
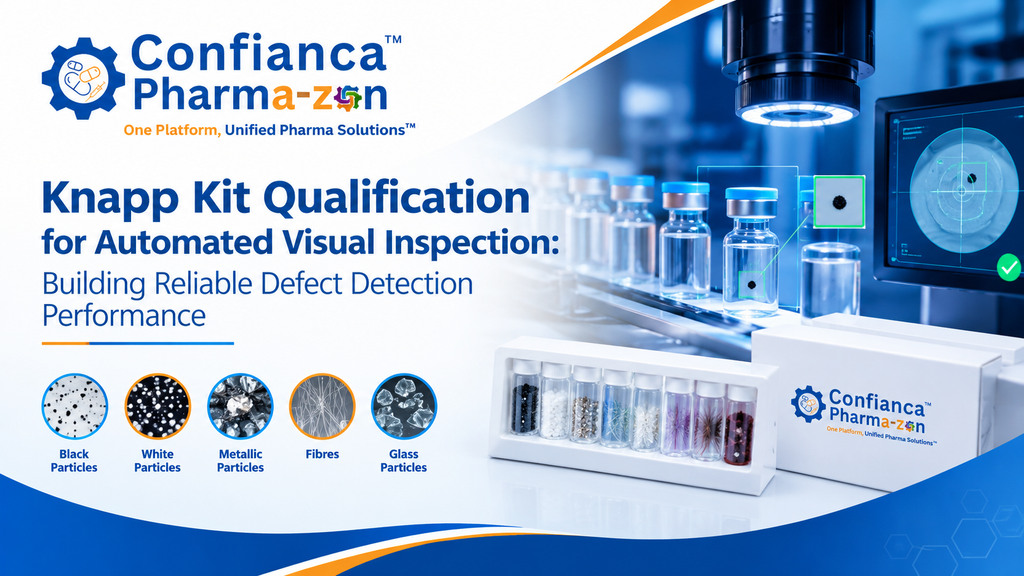
A. Black particles
Black particles can be useful challenges for evaluating contrast and detection capability under appropriate illumination conditions.
B. White particles
White or light-coloured particles may present different detection challenges depending on the product background and container characteristics.
C. Metallic particles
Metallic particles may have reflective properties that influence how they appear under different illumination and viewing conditions.
D. Fibres
Fibres can be challenging because their length, orientation, thickness and movement may influence detection.
E. Glass particles
Glass-related challenges may help evaluate the detection of transparent or partially transparent particulate matter.
The challenge set should be appropriate to the product and inspection system. One defect collection should not automatically be considered representative of every pharmaceutical product.
4. Important Parameters When Selecting a Knapp Kit
The selection of a suitable Knapp kit should involve more than checking the number of supplied samples.
Particle size
The size range should be appropriate to the intended qualification objective.
Particle material
Different materials may have different optical properties and detection characteristics.
Particle colour
Black, white and metallic particles provide different visual challenge conditions.
Container compatibility
Challenge samples should be suitable for the intended vial, ampoule, cartridge or syringe format.
Traceability
Each challenge sample should have an identifiable reference and associated documentation.
Certification and supporting records
Review available particle sizing records, material information, certificates and applicable qualification documentation.
Reproducibility
The challenge configuration should support consistent testing under defined conditions.
5. Developing an Automated Visual Inspection Qualification Protocol
A documented protocol provides a controlled framework for evaluating machine performance.
Step 1: Define the qualification objective
Specify whether the study evaluates initial qualification, machine modification, periodic performance or requalification.
Step 2: Identify the machine configuration
Record equipment identification, software version, camera arrangement, lighting configuration and relevant operating parameters.
Step 3: Select representative challenge samples
Include suitable defect categories and sample configurations based on the product and qualification objective.
Step 4: Establish inspection conditions
Define conveyor speed, container orientation, rotation, illumination, image acquisition settings and other relevant parameters.
Step 5: Define acceptance criteria
Establish acceptance criteria before executing the qualification study.
The criteria should consider defect categories, the number of challenges, repeatability and the intended use of the inspection system.
Step 6: Execute the challenge study
Run the samples under approved conditions and record the machine response for each challenge.
Step 7: Evaluate detection performance
Analyse accepted and rejected containers, false rejects, missed defects and any relevant defect-specific trends.
Step 8: Review and approve the qualification report
Document deviations, investigation outcomes and the final qualification conclusion.
6. Understanding Detection Performance and False Rejection
Automated inspection performance cannot be evaluated by detection rate alone.
Two important parameters are:
Detection performance: The ability of the machine to identify the intended challenge defects.
False rejection: The rejection of acceptable containers that do not contain the targeted defect.
A machine with a high detection rate but an excessive false rejection rate may create operational inefficiencies.
Similarly, a low false rejection rate is not sufficient if important defects are missed.
Manufacturers should evaluate both parameters within a defined and scientifically justified qualification strategy.
Results should also be analysed by defect category rather than relying exclusively on an overall percentage.
7. Common Challenges During Automated Inspection Qualification
Several factors can influence qualification results.
Container orientation
The position of a particle within the container may affect visibility.
Particle movement
Particles may move during container rotation, affecting the inspection image.
Illumination conditions
Light intensity, background and reflection can influence defect visibility.
Machine speed
Higher operating speeds may affect image acquisition and inspection performance.
Product characteristics
Product colour, turbidity, viscosity and container geometry may influence inspection conditions.
Sample integrity
Challenge samples must remain representative throughout the qualification exercise.
Each of these factors should be evaluated according to the machine design and intended inspection application.
8. Documentation Required for an Effective Qualification
An inspection qualification report should provide a clear record of what was tested and what was demonstrated.
Recommended documentation includes:
- Approved qualification protocol.
- Equipment identification and configuration.
- Challenge sample identification.
- Particle type and available sizing documentation.
- Machine operating parameters.
- Individual challenge results.
- Detection and false rejection data.
- Deviations and investigations.
- Acceptance criteria assessment.
- Final approval and conclusion.
Traceability is especially important when qualification records are reviewed during internal audits or regulatory inspections.
9. Maintaining Automated Inspection Performance After Qualification
Initial qualification is not the end of the inspection lifecycle.
Manufacturers should establish ongoing monitoring and change-control processes.
Relevant activities include:
- Periodic inspection performance evaluation.
- Review of defect-specific rejection trends.
- Monitoring of missed defects.
- Evaluation after machine maintenance.
- Assessment following software or hardware changes.
- Periodic review of challenge sample condition.
- Requalification based on documented risk and change-control requirements.
The frequency and extent of these activities should be established through an appropriate quality system.
10. How Confianca Pharmazon Supports Visual Inspection Qualification
Confianca Pharmazon offers pharmaceutical visual inspection-related products and solutions to support quality control and inspection qualification activities.
Our product portfolio includes visual inspection Knapp kits and related pharmaceutical inspection solutions.
Our focus includes:
- Particle challenge materials.
- Black, white and metallic particle sets.
- Different particle size configurations.
- Visual inspection qualification support.
- Technical documentation.
- Customized challenge kit requirements.
The selection of a suitable kit should be based on the intended inspection application and the customer’s documented qualification requirements.
Frequently Asked Questions
1. What is Knapp Kit Qualification?
It is an evaluation approach using representative challenge defects to assess visual inspection performance under defined conditions.
2. Can a Knapp kit be used for automated inspection machines?
Suitable challenge kits can support automated inspection machine performance evaluation when their design and configuration are appropriate for the intended application.
3. Which particles should be included in a challenge kit?
Common challenge categories include black, white and metallic particles, as well as other representative defect materials according to the inspection objective.
4. Why should particle size documentation be reviewed?
Particle size documentation helps establish traceability and supports interpretation of challenge results.
5. Is initial machine qualification sufficient?
No. Ongoing performance monitoring, change control and risk-based requalification are important parts of the inspection lifecycle.
6. What is the difference between detection rate and false rejection rate?
Detection rate measures the identification of intended defects, while false rejection rate measures the rejection of acceptable containers.
Conclusion
Automated visual inspection plays an important role in pharmaceutical manufacturing, but equipment installation alone cannot demonstrate reliable inspection performance.
A structured Knapp Kit Qualification strategy helps manufacturers evaluate machine capability using representative defects, controlled operating conditions and documented acceptance criteria.
By combining suitable challenge materials, scientifically designed protocols and ongoing performance monitoring, pharmaceutical manufacturers can strengthen their visual inspection programmes.
Confianca Pharmazon supports pharmaceutical manufacturers with visual inspection Knapp kits and related product solutions designed to meet their inspection requirements.
Looking for pharmaceutical Knapp kits or customized visual inspection challenge materials? Contact Confianca Pharmazon.